Enhancing Efficiency with Mud and Stone Separators in Industrial Applications
Sep 25,2026
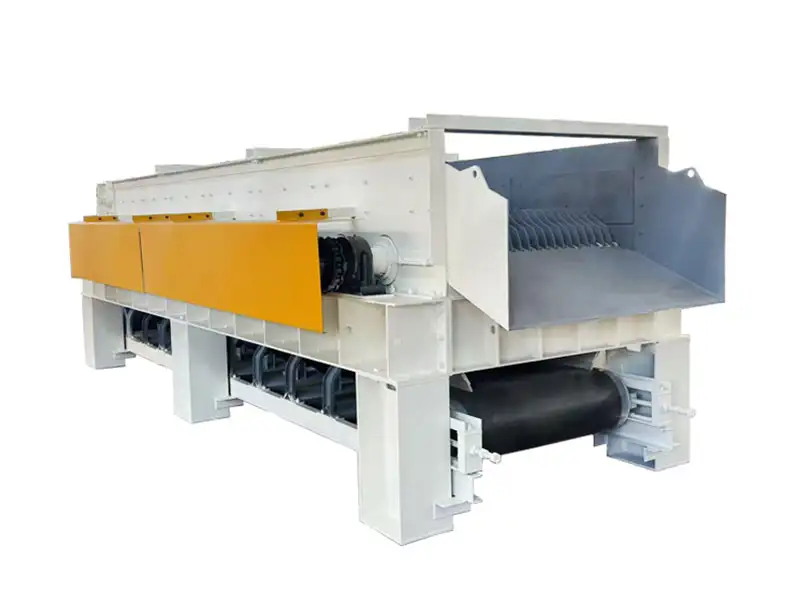
In industrial applications, the management of mud and stone separation is crucial for optimizing processes and ensuring the quality of end products. Mud and stone separators are specialized equipment designed to efficiently separate solid particles, such as mud and stones, from liquids or slurries. This process is essential in various industries, including mining, construction, and wastewater treatment, where the presence of solids can hinder operations and reduce product quality.
The primary function of mud and stone separators is to enhance the clarity and purity of liquids by removing unwanted solid materials. These separators utilize various techniques, including mechanical, hydraulic, and gravity-based methods, to achieve effective separation. Mechanical separators often employ screens or filters to capture larger particles, while hydraulic separators leverage differences in density to allow lighter materials to flow away from heavier solids. This versatility enables operators to select the most suitable technology according to the specific requirements of their processes.
One of the key benefits of using mud and stone separators is their ability to improve operational efficiency. By removing solid contaminants, these devices help maintain the performance of downstream equipment, reducing wear and tear and minimizing downtime. In industries such as mining, the presence of mud and stones can lead to significant operational issues, including clogged pipelines and inefficient processing. Implementing effective separation solutions can greatly enhance productivity and reduce maintenance costs.
Additionally, mud and stone separators play an essential role in environmental management. Proper separation of solids from liquids minimizes the environmental impact of industrial processes. For instance, in wastewater treatment, effective separation can prevent the discharge of harmful solids into natural water bodies, thus protecting ecosystems and complying with environmental regulations. Furthermore, recovered materials can often be reused or recycled, contributing to sustainability efforts within the industry.
The applications of mud and stone separators are vast. In the construction industry, these devices are used to manage sediment-laden water during excavation and site preparation, ensuring that only clean water is released into the environment. In the mining sector, they help in processing ore by separating valuable minerals from waste materials. This separation not only enhances resource recovery but also reduces the overall environmental footprint of mining operations.
In conclusion, mud and stone separators are invaluable components in various industrial processes. Their ability to efficiently remove solid contaminants from liquids enhances operational efficiency and environmental compliance. By understanding the functionality and potential applications of these separators, industries can optimize their processes, reduce costs, and promote sustainability. Investing in effective separation technology is a strategic move for organizations aiming to improve productivity while adhering to environmental standards.
The primary function of mud and stone separators is to enhance the clarity and purity of liquids by removing unwanted solid materials. These separators utilize various techniques, including mechanical, hydraulic, and gravity-based methods, to achieve effective separation. Mechanical separators often employ screens or filters to capture larger particles, while hydraulic separators leverage differences in density to allow lighter materials to flow away from heavier solids. This versatility enables operators to select the most suitable technology according to the specific requirements of their processes.
One of the key benefits of using mud and stone separators is their ability to improve operational efficiency. By removing solid contaminants, these devices help maintain the performance of downstream equipment, reducing wear and tear and minimizing downtime. In industries such as mining, the presence of mud and stones can lead to significant operational issues, including clogged pipelines and inefficient processing. Implementing effective separation solutions can greatly enhance productivity and reduce maintenance costs.
Additionally, mud and stone separators play an essential role in environmental management. Proper separation of solids from liquids minimizes the environmental impact of industrial processes. For instance, in wastewater treatment, effective separation can prevent the discharge of harmful solids into natural water bodies, thus protecting ecosystems and complying with environmental regulations. Furthermore, recovered materials can often be reused or recycled, contributing to sustainability efforts within the industry.
The applications of mud and stone separators are vast. In the construction industry, these devices are used to manage sediment-laden water during excavation and site preparation, ensuring that only clean water is released into the environment. In the mining sector, they help in processing ore by separating valuable minerals from waste materials. This separation not only enhances resource recovery but also reduces the overall environmental footprint of mining operations.
In conclusion, mud and stone separators are invaluable components in various industrial processes. Their ability to efficiently remove solid contaminants from liquids enhances operational efficiency and environmental compliance. By understanding the functionality and potential applications of these separators, industries can optimize their processes, reduce costs, and promote sustainability. Investing in effective separation technology is a strategic move for organizations aiming to improve productivity while adhering to environmental standards.
